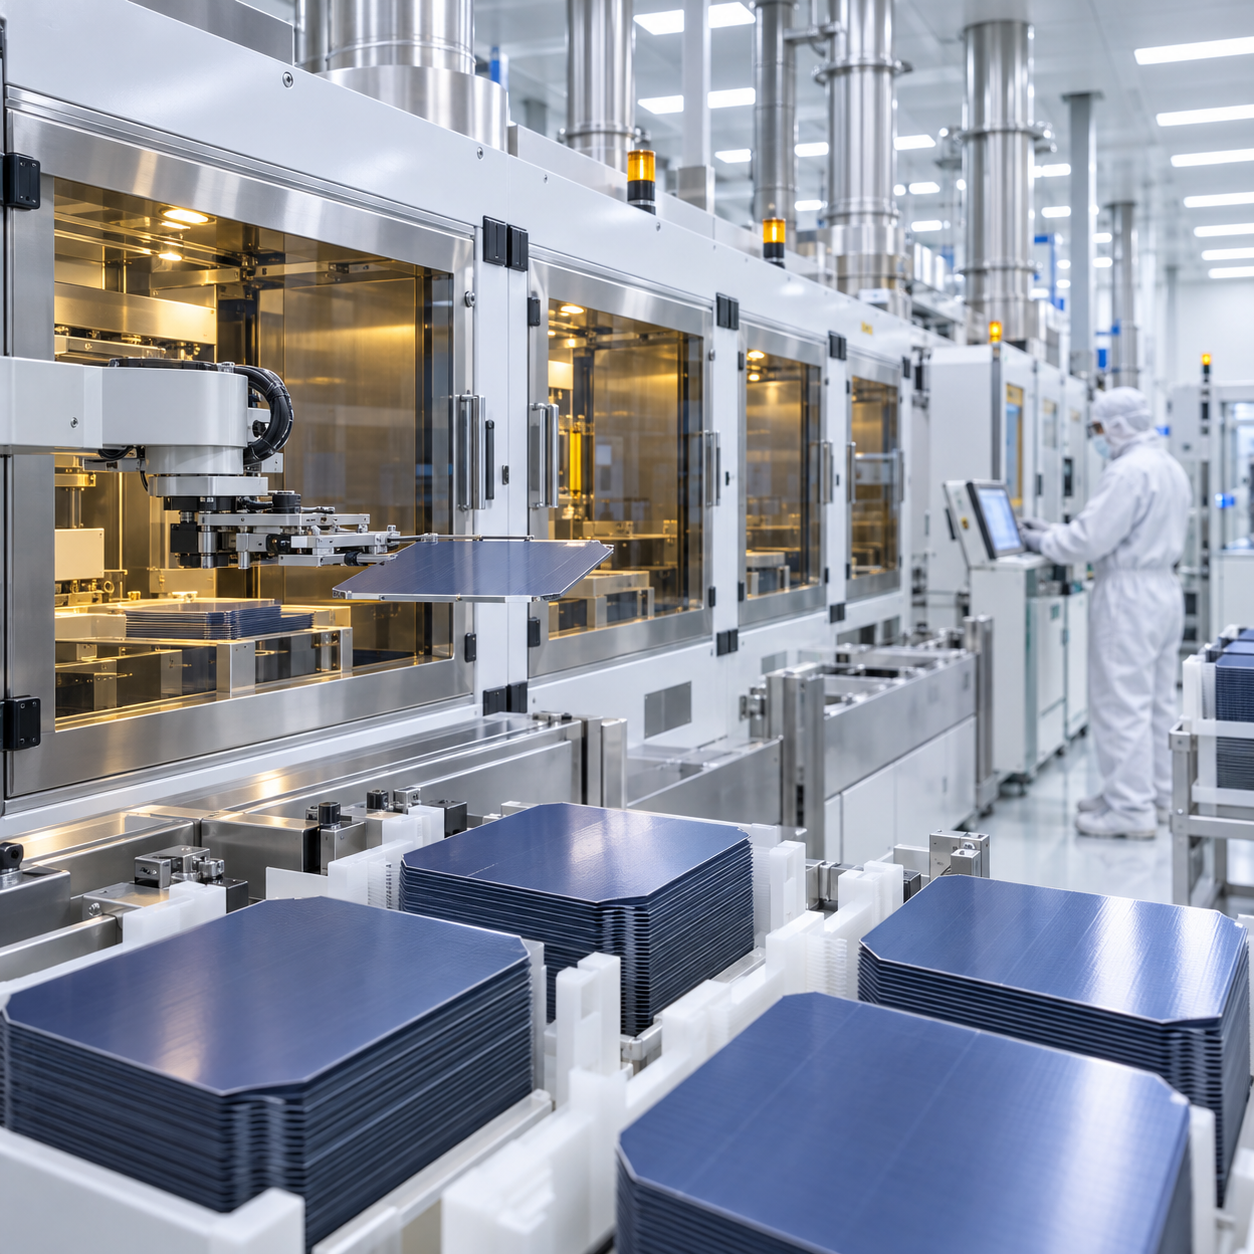
Nitric acid is used as an oxidizing component in selected acidic silicon-wafer texturing systems for photovoltaic manufacturing. Performance depends on wafer type, saw damage, companion chemistry, bath loading, temperature, mass transfer and the target optical and electrical surface. These processes may involve extremely hazardous mixed acids, so chemistry cannot be transferred from a paper or another line without formal engineering and safety validation. This article addresses nitric acid purity, monitoring and industrial supply. It does not provide a formulation, mixing sequence, temperature or etch time.
For B2B qualification, assign purchasing, quality, engineering, operations, logistics and EHS ownership before the first commercial delivery. Approve the specification, analytical methods, sampling point, retained-sample period, storage conditions, transfer equipment, deviation response and release authority in writing. Compare representative lots under controlled conditions and record process performance, mass balance, waste, equipment observations and final quality. This separates raw-material variation from water, equipment, operator or analytical changes. Review the chain from supplier release through carrier, package, receiving connection and day tank because contamination or misidentification can occur after final analysis. Reconcile ordered, received, stored and consumed quantities and investigate unexplained differences. Supplier scorecards should cover documentation accuracy, delivery condition, corrective-action quality and change notification as well as price. Qualify an alternate source before a disruption using the same methods and process criteria. When buyer and supplier results differ, review sample representativeness, temperature, calibration, detection limits and uncertainty before deciding disposition. Confirm emergency contacts, unloading hours and stop-work authority for every shipment. Include maintenance and warehouse teams in post-trial review because they often identify seal, vent, hose or handling issues not visible in a certificate of analysis. Close qualification with an authorized report, approved supplier status and a defined routine-monitoring plan. Nitric acid is a strong oxidizer and corrosive chemical; the current SDS, local law and site procedures control segregation, handling, ventilation, exposure control and emergency response.
Define the wafer and surface objective
Identify silicon type, wafer thickness, sawing method, incoming damage, required etch removal, texture, reflectance and downstream cell architecture. Establish dimensional, optical, surface and electrical acceptance criteria before evaluating a new acid lot or supplier.
Use research without copying a recipe
A Solar Energy Materials and Solar Cells study examined nitric-acid-containing mixtures for texturing different sawn silicon wafers. Its results show that wafer history and complete chemistry influence texture; they are not universal production instructions.
Create a process-specific nitric acid specification
Set assay, water, particles, residue, chloride, sulfate and individual metals at limits supported by wafer risk and analytical capability. State methods, detection limits and units. A nominal purity grade is not enough when trace contamination can affect lifetime, recombination or yield.
Test multiple packages and lots
Compare several commercial lots using representative wafers and matched process conditions. Include samples from the first and last portion of packages where justified. Record container, closure and connection because delivery hardware can add particles or metals after supplier release.
Monitor the operating bath as a system
Track acid balance, dissolved silicon, water, temperature, loading and process age with validated controls. Incoming nitric acid release does not replace bath analysis. Define replenishment, hold and retirement rules and prevent operators from correcting drift through undocumented additions.
Link chemistry to wafer performance
Trend etch removal, weight loss, surface morphology, reflectance, breakage, residual contamination and downstream cell results. Investigate shifts using bath history, acid lot, wafer lot, water quality and tool maintenance instead of assigning cause from one metric.
Govern mixed-acid and NOx risk
Use closed compatible tools, automated dosing, exhaust, scrubbers, containment and interlocks designed for the complete chemistry. Prevent backflow and incorrect connection. The current SDS and site process-hazard analysis must address oxidizing acid, toxic reaction products and any companion chemical hazards.
Plan spent-bath treatment
Characterize dissolved silicon, nitrate, companion species and trace metals before selecting recovery or treatment. Monitor abatement and wastewater systems as production loading changes. Process economics should include chemical loss, rinsing, ventilation, waste and downtime.
Control supplier changes and continuity
Require notification for site, route, purification, filtration, analytical method, filling environment and package changes. Use a defined bridging plan and production hold point. Qualify alternate supply under the same wafer and bath criteria before an emergency.
Prepare a photovoltaic supply inquiry
Provide complete impurity limits, methods, package, annual volume, destination and change-control expectations without sharing the proprietary etch recipe. Review the Hiacid nitric acid supply page, then ask whether the required documented grade can be offered.
Related nitric acid resources
- Nitric Acid for Titanium Pickling Quality Control
- Nitric Acid Supply for Dairy CIP Systems
- Nitric Acid for NdFeB Magnet Recycling Trials
Frequently asked questions
Is all high-assay nitric acid suitable for solar wafer texturing?
No. Trace metals, particles, residue, package and full process compatibility must be qualified.
Does this guide provide an etching formula?
No. Mixed-acid conditions require proprietary process validation and formal hazard controls.
Why link acid lots to downstream cell results?
Surface chemistry can affect reflectance, contamination, recombination and yield beyond the wet bench.
What supplier changes may require requalification?
Changes to site, route, purification, methods, filtration, filling or packaging can alter critical quality.