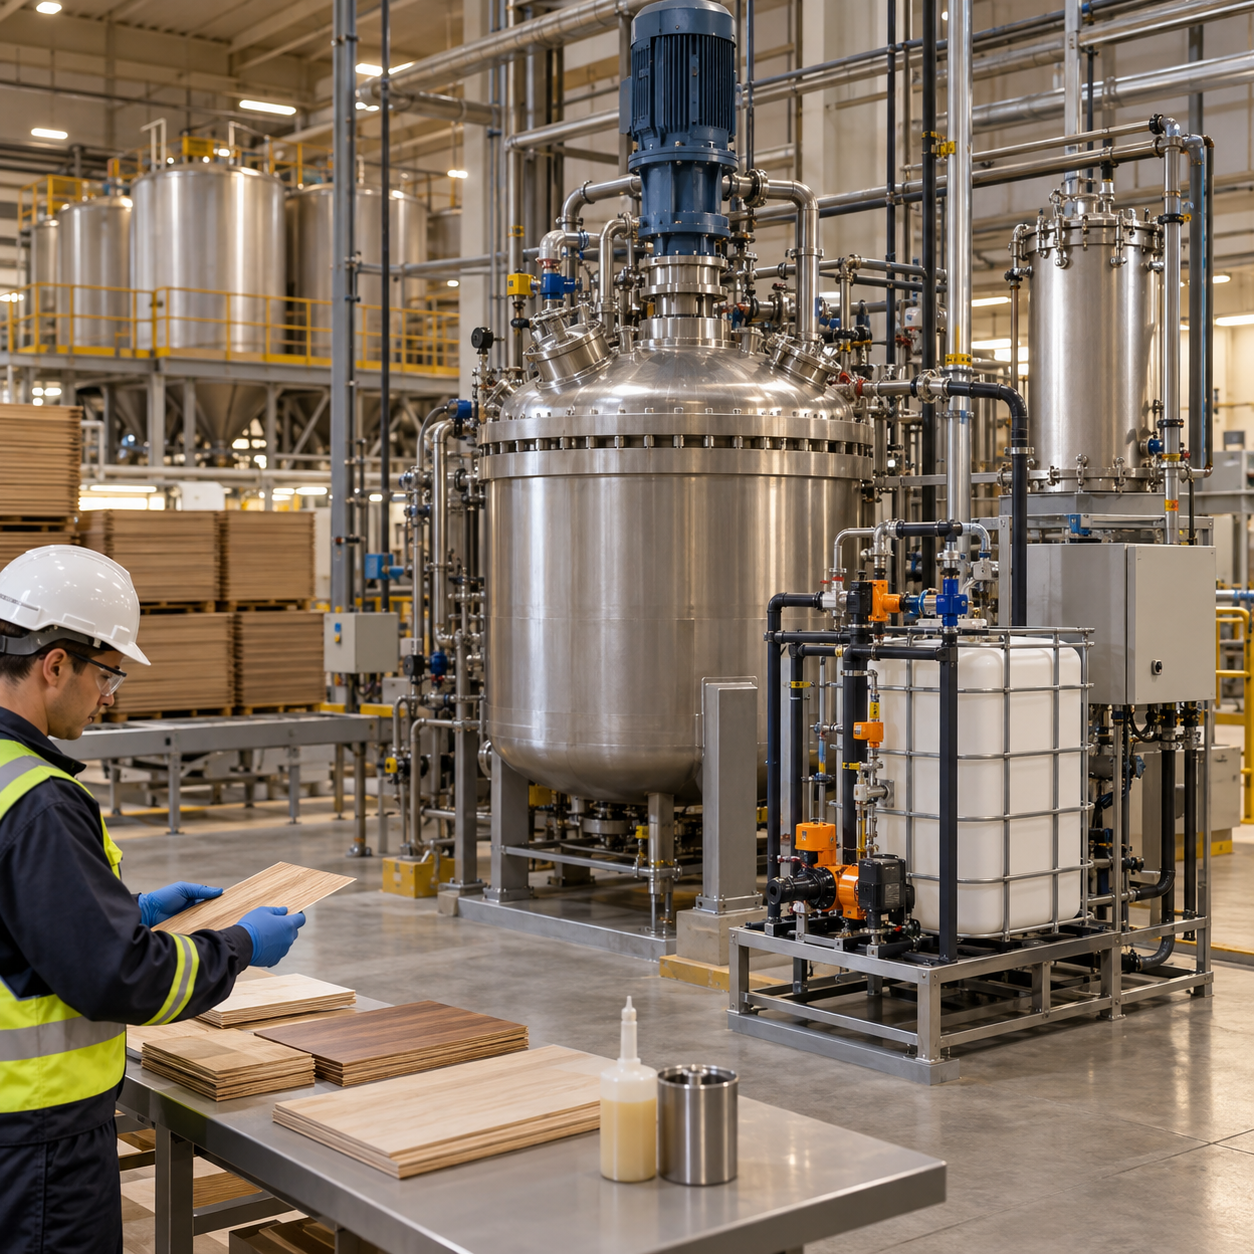
Wood adhesive resin manufacture can require controlled pH adjustment during synthesis, finishing or application, and formic acid may be evaluated as one of several acidifying agents. The effect is resin-specific: buffering, solids, temperature, catalyst system, storage age and wood furnish can all change the response. An acid that reaches a target pH can still affect viscosity, cure profile, pot life, emissions or bond durability. Procurement therefore needs more than acid concentration and price. It needs a validated operating window, impurity controls, safe closed dosing and supplier change management. This article supports industrial qualification and intentionally does not provide a resin formulation or dosing recipe.
For industrial qualification, assign purchasing, quality, engineering, operations, logistics and EHS ownership before the first commercial delivery. Approve the formic acid concentration, analytical methods, sample point, retained-sample period, storage conditions, transfer equipment, deviation response and release authority in writing. Compare representative lots under controlled conditions and record process performance, mass balance, waste, equipment observations and final product quality. This separates raw-material variation from changes in water, feedstock, equipment, operator or analytical method. Review the chain from supplier release through carrier, package, receiving connection and day tank because contamination or misidentification can occur after final analysis. Reconcile ordered, received, stored and consumed quantities and investigate unexplained differences. Supplier scorecards should cover documentation accuracy, delivery condition, corrective-action quality and change notification as well as price. Qualify a contingency source before a disruption using the same methods and process criteria. When buyer and supplier results differ, review sample representativeness, temperature, calibration, detection limits and uncertainty before deciding disposition. Confirm emergency contacts, unloading hours and stop-work authority for every shipment. Include maintenance and warehouse teams in the post-trial review because they often identify seal, vent, hose or handling issues not visible on a certificate of analysis. Close qualification with an authorized report, approved-supplier status and a defined routine-monitoring plan. The NIH PubChem record for formic acid provides broad identity and hazard context; the current SDS, local law and site procedures remain controlling.
Define the resin and process objective
State whether formic acid is being screened for synthesis control, final adjustment, catalyst preparation or another documented function. Identify resin family, solids, buffer capacity, temperature and the point at which pH is measured.
Do not treat pH as the only endpoint
Track viscosity, gel time, storage stability, cure behavior, bond strength, water resistance and emissions where relevant. A published ACS Omega study on wood adhesive systems illustrates that formic acid may appear in resin pH adjustment, but plant formulations still require their own validation.
Design controlled laboratory and pilot trials
Use the production resin, actual wood species or panel furnish, representative pressing conditions and predetermined acceptance criteria. Compare alternative acidifying strategies and include aged resin because freshly made laboratory material may hide stability problems.
Measure at representative locations
Verify pH and temperature after adequate mixing and at the process point that governs quality. A local probe reading near the injection point can misrepresent the full batch and encourage excessive addition.
Engineer closed and fail-safe dosing
Use compatible storage, calibrated metering, backflow prevention, mixing, containment and interlocks. Review loss of flow, stuck valve, empty package, sensor drift and concentrated slug scenarios.
Protect workers and equipment
Formic acid is corrosive and concentrated vapor can be hazardous. Use the current SDS, ventilation, compatible PPE, eyewash, shower and spill response. Confirm compatibility of tanks, pumps, seals, hoses and reactor materials for the delivered concentration.
Specify quality that protects the resin
Control assay, water, color, nonvolatile residue, metals and organic impurities where trials show sensitivity. Require methods and reporting limits capable of demonstrating the specification rather than accepting vague typical values.
Link acid lots with panel performance
Record supplier lot, receiving results, resin batch, process settings and finished-panel data. Trend them together so raw-material effects can be distinguished from wood moisture, press temperature, catalyst or operator changes.
Qualify supply before routine production
Approve the manufacturing site, package, COA, SDS, retained-sample plan, deviation response and change-notification terms. Conduct comparison trials across more than one acid and resin lot before reducing incoming testing.
Prepare an adhesive-resin inquiry
Provide concentration, impurity limits, package, annual volume, destination and quality-document needs. Review the Hiacid formic acid page, then request a documented industrial quotation.
Related formic acid resources
- Food-Grade Formic Acid Supply and Compliance
- Formic Acid for Sodium Formate Deicer Production
- Formic Acid for Transparent Wood Film Manufacturing
Frequently asked questions
Can one formic acid dose work for every wood resin?
No. Resin chemistry, buffering, solids, temperature and process stage all affect the response.
Why monitor more than pH?
Viscosity, cure, pot life, emissions and bond durability can change even when the target pH is reached.
Should dosing be manual?
Industrial systems should use a risk-reviewed, compatible and calibrated closed dosing arrangement with safeguards.
Which formic acid impurities may matter?
Water, color, residue, metals and organic impurities should be assessed against resin and finished-panel performance.