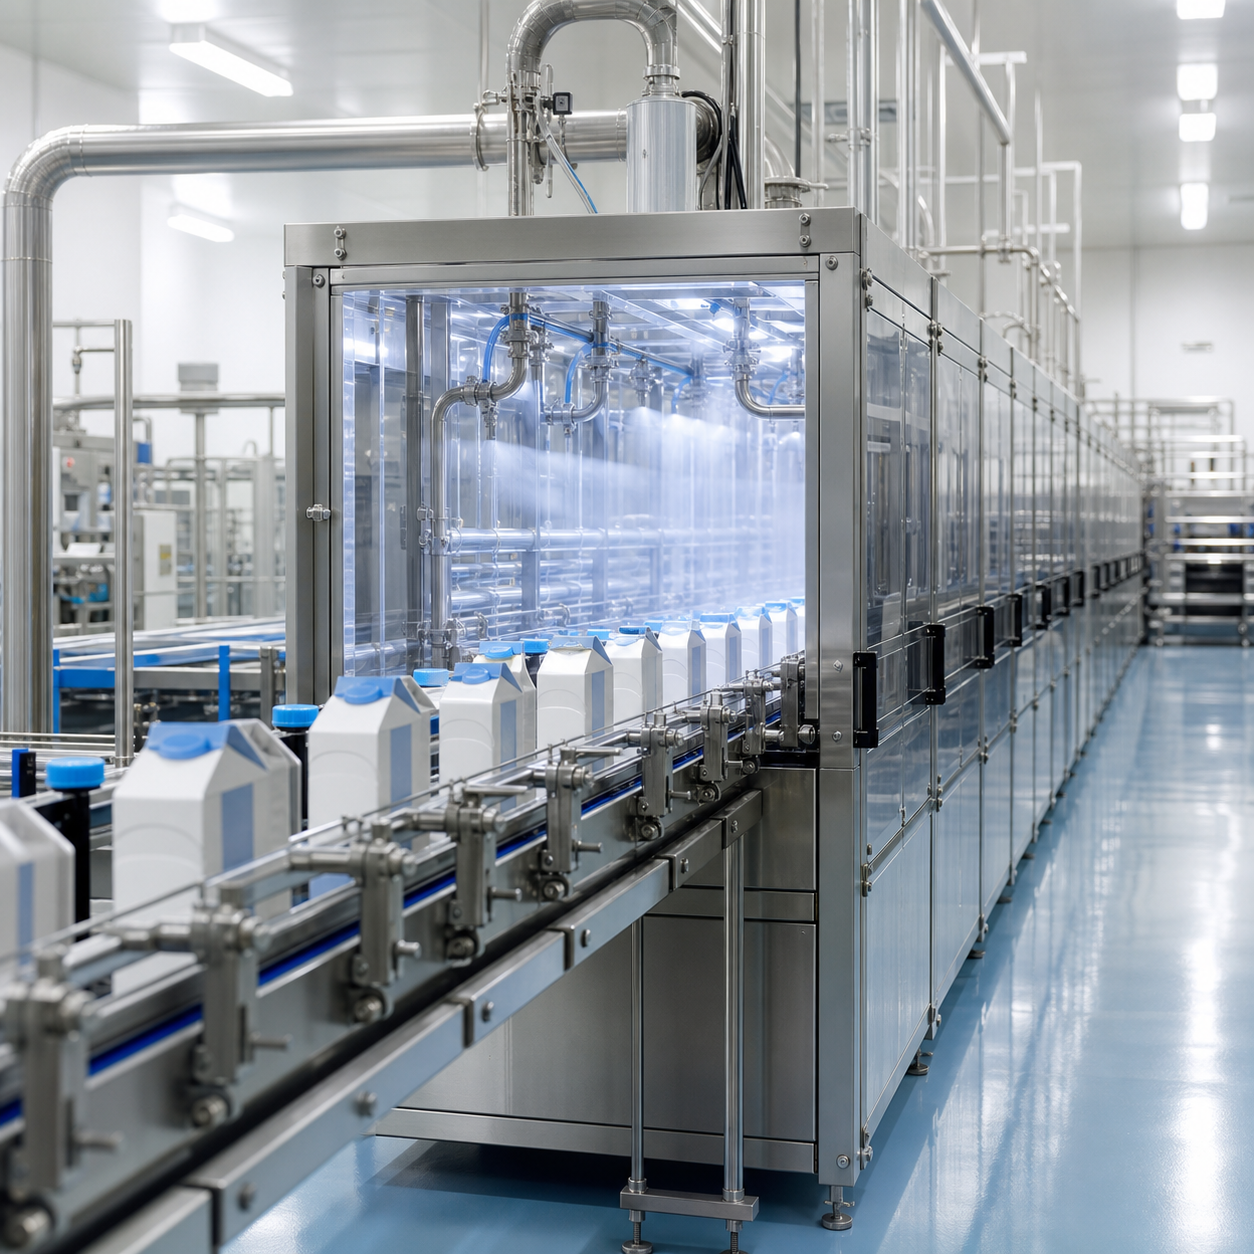
Hydrogen peroxide is used in selected aseptic packaging systems to sterilize packaging material or controlled equipment surfaces before filling. The chemical is only one element of a validated scheduled process. Commercial sterility depends on peroxide concentration, application method, contact, temperature, sterile air, drying, packaging geometry, initial bioburden, equipment condition and automatic safeguards. A supplier cannot define the operating process for the food producer, and a plant cannot assume that changing peroxide grade or concentration is equivalent without review. The applicable regulatory authorization, process filing and process-authority documentation must be identified for the specific packaging material, food and jurisdiction. Procurement should translate that approved process into a raw-material specification covering assay, relevant impurities, stabilizer profile, lot documentation, packaging and change notification. Operations should trend peroxide consumption, concentration, deposition or bath level, heating conditions and residual results. Deviations from critical factors require the plant’s approved disposition procedure rather than informal adjustment.
For B2B implementation of Hydrogen Peroxide for Aseptic Packaging Sterilization, assign ownership across purchasing, quality, production, engineering, logistics and EHS before the first delivery. Approve the receiving test, compatible handling system, deviation response, retained-sample period and supplier-change process in writing. This shared control plan helps separate raw-material variation from equipment or operating changes and provides objective evidence for investigations.
Start with the approved scheduled process
Identify the packaging system, material, food category, sterilization method, critical factors and regulatory basis. The validated process—not a generic peroxide claim—sets allowable concentration, temperature, contact and drying conditions. Changes must be reviewed by qualified regulatory and process authorities.
Define raw-material requirements from validation
Specify concentration range, impurity and stabilizer characteristics that matter to delivery, equipment and residual performance. Review multiple supplier lots in the operating system. If a stabilizer or production route changes, assess deposits, sensors, drying and residuals before routine acceptance.
Control application and contact
Monitor the filed critical parameters for immersion, spray, roller, fog or other approved application. Verify nozzle or applicator condition, coverage, bath level or deposition and peroxide consumption. Difficult folds, closures and shadowed surfaces may require specific validation evidence.
Integrate heat and sterile air
Many systems combine peroxide with heat or hot sterile air. Temperature, airflow, humidity and residence time can affect microbial reduction and peroxide removal. Calibrate instruments and challenge automatic guards at the approved frequency; a displayed setpoint alone does not prove delivered conditions.
Verify drying and residual control
Define the approved method, sampling location, timing and acceptance criterion for peroxide residuals. Trend results by line, package and operating condition. A low average cannot excuse a high result at a difficult location, and residual testing does not replace sterilization validation.
Manage packaging material quality
Control incoming packaging bioburden, storage, handling and damage. Packaging changes in coating, thickness, forming behavior or surface energy can alter wetting and drying. Include packaging suppliers in change notification and deviation investigations.
Use regulatory references correctly
The US FDA aseptic processing and packaging inspection guide describes systems using hydrogen peroxide and heat and identifies monitoring topics such as consumption, concentration, application, heating and residuals. Companies must confirm the regulations and filings that apply to their own product and market.
Protect workers and equipment
Use enclosed application, ventilation, interlocks, compatible materials, spill controls and current SDS instructions. The NIOSH hydrogen peroxide entry provides occupational-hazard context. Food compliance does not eliminate oxidizer, corrosion or exposure risks.
Qualify supply continuity
Review manufacturing site, quality system, lot traceability, COA, retained samples, complaint handling and business continuity. Prequalify alternates using the same specification and line validation plan before a disruption. Do not make emergency substitutions directly into commercial production.
Prepare an aseptic-grade RFQ
State intended application, required concentration and grade, impurity or stabilizer controls, packaging, annual volume, documents, destination and change-notification period. Review the Hiacid hydrogen peroxide supply page and storage guide, then request qualification information.
Related hydrogen peroxide resources
- Hydrogen Peroxide Storage and Material Compatibility Guide
- High-Purity Hydrogen Peroxide for Semiconductor Cleaning
- Hydrogen Peroxide for Cyanide Destruction in Gold Mining
Frequently asked questions
Does hydrogen peroxide alone guarantee commercial sterility?
No. Sterility depends on the complete validated packaging process and all identified critical factors.
Can the supplier choose the operating concentration?
No. The approved process and applicable regulatory basis determine the operating requirements.
Why monitor peroxide residuals?
Residual testing verifies the approved removal conditions and applicable acceptance requirement.
Can packaging material changes affect sterilization?
Yes. Surface, geometry, coating and forming changes can affect wetting, contact and drying.